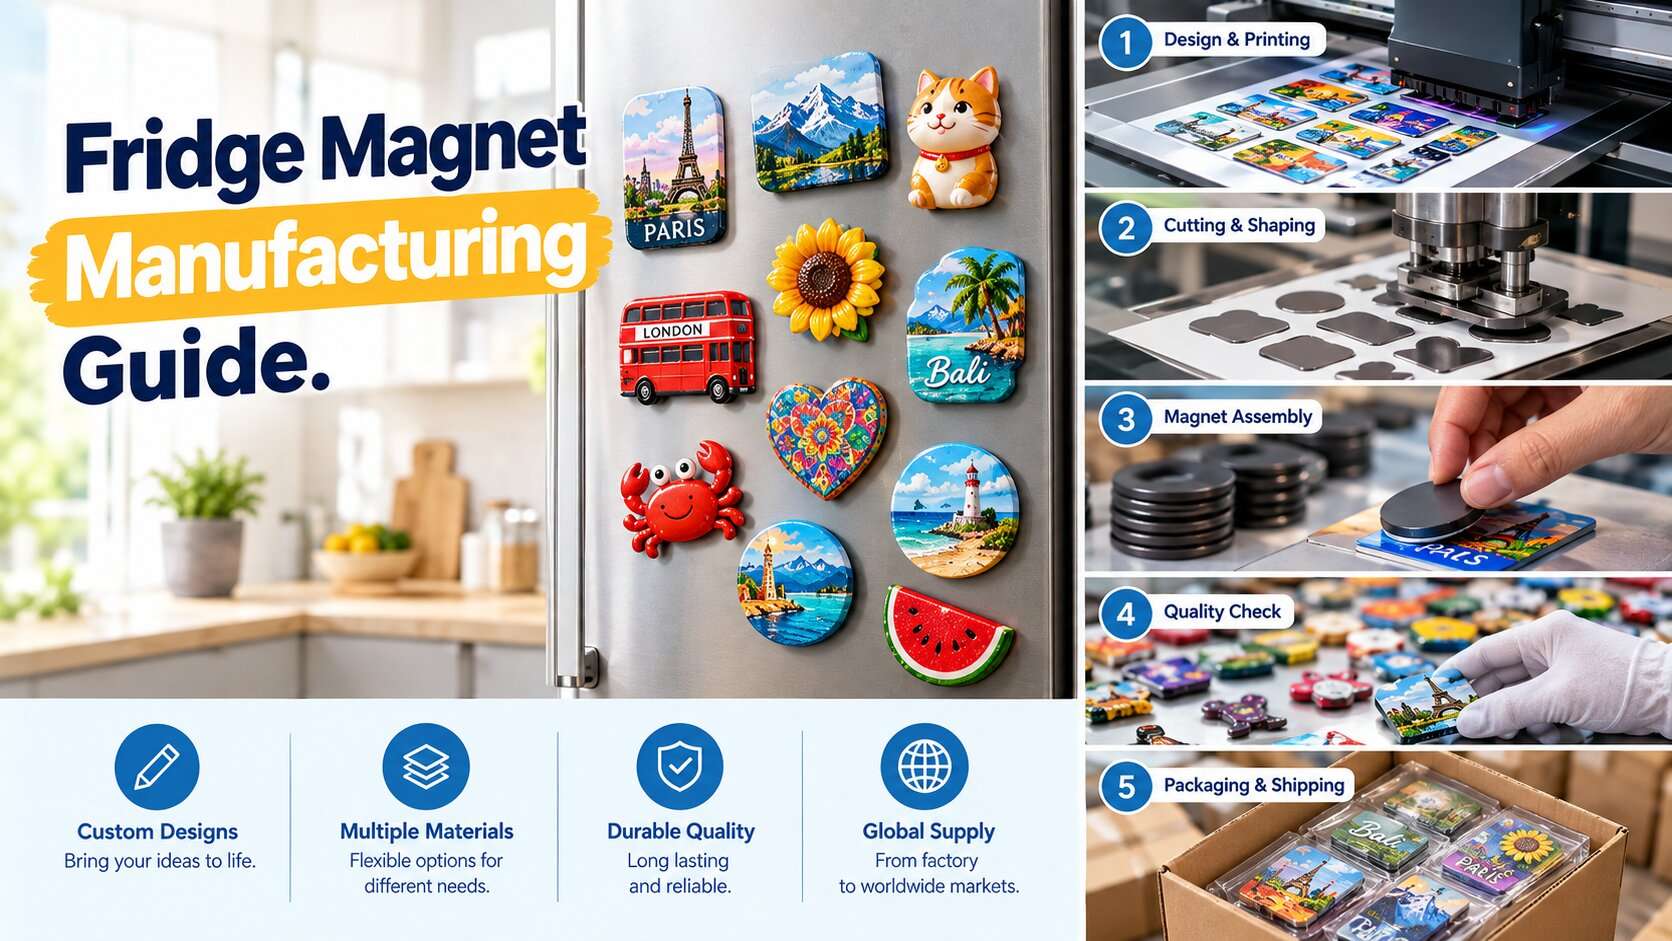
A fridge magnet looks simple. But making one that stays flat, holds on a real door and clears export checks takes more decisions than most buyers expect. This fridge magnet manufacturing guide covers materials, the main production routes, equipment, quality control, safety rules and costs. We supply fridge magnet at wholesale rate to retailers and distributors, so the guide is written for people who make, specify or buy magnets in volume.
A fridge magnet is a decorative layer bonded to a magnetic base. The base is usually flexible ferrite sheet, or a small rigid magnet set behind a 3D piece. Four production routes cover almost every product on the market:
| Route | Best for | Tooling | Main cost driver |
|---|---|---|---|
| Flat printed flexible magnet | Photo-style artwork, promotions | Cutting die or laser/CNC file | Print method, shape, finish |
| Epoxy or resin dome | Glossy, raised-lens look on printed art | Dispensing rig, no mold | Resin dosing, cure time, scrap |
| 3D soft PVC or polyresin | Collectible shapes, souvenirs | Molds, one per design | Mold cost spread over the MOQ |
| Wood, acrylic or metal | Premium and logo-led pieces | Laser files or stamping dies | Finish type, weight, scrap rate |
Flexible sheet is ferrite powder held in a polymer binder. It is typically formed by calendering or extrusion. One vinyl-faced sheet datasheet lists about 90% ferrite powder to 10% binder.
The sheet is then magnetized as alternating north-south stripes on one face only. That is why a fridge magnet grips on one side and leaves the print side nearly inert. Pole spacing matters. Supplier data shows anywhere from 2 to 60 poles per inch, and denser poles give higher holding force. The datasheet above specifies a pole pitch of 1.5–2.5 mm.
Isotropic sheet suits everyday decorative use.
Anisotropic sheet is stronger and used where holding force matters. One 1.0 mm anisotropic sheet is rated at about 130 g/cm². That is a lab figure on steel, so real doors will give less.
Typical flexible thickness is 0.3–1.0 mm. Thicker sheet holds more but costs more and weighs more in the carton. Temperature matters too. The datasheet sheet is rated −20 °C to 80 °C, with performance dropping above that. Check the rating for magnets that will sit near ovens or dishwashers.
Rigid magnets sit behind 3D pieces. Ferrite discs are the safe default. Neodymium holds far more per gram, but it is brittle, and swallowing several is a serious hazard, as the compliance section explains.
Check the door as well as the magnet. Whether a “stainless” door grips depends on the alloy. Magnetic grades hold, while many austenitic grades hold weakly or not at all.
Start from the artwork and the volume, not the machine.
Photographic or gradient artwork fits flat printed or domed magnets.
Sculpted, collectible shapes need molds. Soft PVC and polyresin are the usual choices.
Premium or logo-led pieces suit laser-engraved wood and acrylic, or metal with filled color.
Short runs favor digital print and laser. Molds only pay back at volume.
MOQ follows the route. One export factory lists 480 pieces per design for printed and laser products, and 1,440 for metal and plastic. The same listing notes that printed designs should normally fill a full A4 sheet. Printed designs are gang-run on sheets, while molded designs carry the tooling.
Prepress. Use vector or high-resolution files with bleed, cut lines and Pantone references. Low-resolution art is a common cause of rejected samples.
Printing. Digital suits short runs, offset suits long runs, and screen suits bold, few-color designs.
Lamination and bonding. The print is laminated and bonded to the magnetic base, with heat-activated adhesive common in production.
Cutting. Use steel-rule dies for repeat shapes, or CNC knife or laser for custom outlines. Confirm the sheet is laser-safe. One supplier marks its plain sheet unsuitable for laser cutting, and vinyl-containing layers can release corrosive fumes under a laser.
At industrial scale, sheet laminators can apply magnetic film at up to 45 m/min on sheets up to 76 × 102 cm. Optically registered die cutters then cut the shape. Registration is the point of the optical cutter. Manual alignment drifts across a long run.
Curl and edge lift is the defect to design against. Sign-trade practitioners most often blame shrinkage of calendered vinyl and the direction the magnet was rolled, and edge lifting is a recurring complaint. Most reports come from large vehicle magnets. The same mechanics apply to small magnets, especially at rounded corners. Specify dimensionally stable face film, and relax printed stock before lamination. Neither is a guarantee, and one practitioner reported bubbling and curl even after resting the print for two days. Test your exact stack.
A measured dose of clear resin is dispensed onto a printed blank and self-levels into a dome. Suppliers name the resin differently. One describes clear polyurethane, while casting guides describe epoxy. Don’t rely on the label. Put the properties in your spec: non-yellowing, hardness and cure conditions.
The process controls that decide yield are:
Dose: too little leaves a flat dome, and too much runs over the edge.
Level surface: a tilted tray gives lopsided domes.
Dust and bubbles: both are locked in permanently at cure.
Full cure: handle or pack only after the surface is hard.
3D Soft PVC and Polyresin Magnets
The flow is concept sculpt or 3D-printed prototype, then mold, then casting or injection, then cure, trim and paint. One factory process description uses a prototype, a silicone mold, mixed resin and a cast, then magnet attachment.
Three practical points:
Wood, Acrylic and Metal Magnets
Finish drives both look and cost. For metal pieces, a finish comparison shows baked paint fill gives a glossy recessed color, UV printing is fast but flatter, and translucent resin fill carries a high scrap rate.
Two assembly rules apply across these materials:
Glue the magnet after finishing, never before cutting or engraving.
Use two magnets on larger pieces. Place them symmetrically so the hold stays even and the piece doesn’t tilt.
Equipment by Production Scale
| Scale | Typical kit | Where it stops |
|---|---|---|
| Hobby or micro | Press kit with cutter (one retail kit lists around $256, with a photo-paper limit of 157 g/m²), desktop laser | Hundreds of pieces, one or two shapes |
| Small studio | Digital or UV printer, laminator, cutting plotter, dispensing station | Custom shapes in short runs; no 3D molding |
| Industrial | Sheet or roll laminator with magnetic film, optically registered die cutter, molds and paint line | High volume; needs tooling budget and test capability |
Outsource when you need molds, large runs or lab-tested compliance.
Magnet Placement, Holding Force and Adhesives
Full-back sheet grips through friction as well as pull, so it resists sliding better than a small spot magnet.
Set the holding target as a multiple of the piece’s weight, not equal to it. Doors vibrate when slammed. Then validate on painted, textured and stainless doors.
Keep magnets clear of moving parts. On an articulated piece, a magnet near the pivot makes the joint bind against the door.
Let adhesive cure fully. Half-cured epoxy lets go under shear, which shows up as a magnet sliding off the piece in the field.
Quality Control and Common Defects
| Defect | Likely cause | Prevention and check |
|---|---|---|
| Corner curl, edge lift | Film shrinkage, rolling direction, heat | Stable film, flat packing, heat-cycle sample |
| Bubbles under laminate | Trapped air, poor lamination pressure | Lamination setting check, 100% visual on first runs |
| Dome bubbles, dust, overflow | Dosing, tray level, dirty environment | Dose control, cover during cure, edge check |
| Weak hold, sliding | Low-grade or thin sheet, single spot magnet | Pull test on steel plate; test on real doors |
| Magnet detaches | Uncured or wrong adhesive, smooth surface | Cure-time rule, peel and shear test |
| Color mismatch | Profile or ink batch drift | Signed color standard, delta check per batch |
| Paint chipping (3D) | Poor primer or cure | Scratch and drop sample test |
Test at three stages: incoming sheet (thickness and pull), in-process (registration, dome, bond) and pre-shipment (sampled inspection against an agreed AQL plus door tests).
Safety and Compliance for Export Markets
| Requirement | Why it matters | What it hits |
|---|---|---|
| EN 71-1 / toy rules | Sets limits for magnets in toys. A UK alert recorded a magnetic flux index of 57 kG²mm, above the permitted maximum, and the import was rejected and destroyed. | Kids’ sets, small loose magnets |
| Food-imitation rules | Food-shaped fridge magnets were withdrawn for choking risk, with flux index above 50 kG²mm². | Cake, fruit and sweet shapes |
| Phthalates | The same UK alert applied a 0.1% limit on four phthalates combined in plasticised material. | Soft PVC |
| REACH, RoHS, EN 71-3 | A vinyl-faced sheet datasheet states conformity to EN 71-3, REACH and RoHS. | Materials and finishes |
| CPSIA, Prop 65, EU GPSR | Depend on market and end use. The GPSR also covers children’s products that are not toys. | US and EU exports |
Swallowed magnets are the core hazard. Swallowing more than one can block, perforate or damage the intestine. Whether a fridge magnet counts as a toy depends on its design and marketing, and kid-oriented sets get stricter treatment. Ask for test reports on the exact SKU, use an accredited lab, and re-check the rules before each new market, because they change.
Customization options are shape, size, thickness, finish (matte, gloss, dome), magnet strength, and packaging such as sets, backing cards or hangers. Set design also matters. A themed six-piece series sells as a collection but carries six sets of artwork or molds. Our cultural relic fridge magnet range and prehistoric fossil series show how a theme turns into a sellable set.
Where each type sells:
Cost drivers are tooling, print complexity, finish, size, thickness, packaging and freight weight. Published ranges are indicative only:
Worked example (illustrative, not a quote): 5,000 flat vinyl magnets at $0.25–0.50 is $1,250–2,500 before freight. A custom shape at +30–50% pushes that to about $1,625–3,750.
For an accurate RFQ, send:
Then approve a pre-production sample before the full run.
Alloy grade decides it. Some stainless grades are weakly magnetic or not at all, so test on the actual door.
Not automatically. Small magnets, food shapes and soft PVC all carry rules. Buy tested products and keep small magnets away from young children.
Isotropic is fine for light decorative use. Choose anisotropic when you need more hold at the same thickness.
Yes, with a press kit, laser or digital print. It works for hundreds of pieces, not for molded 3D designs or compliance-tested exports.
Published ranges run from about one week for basic runs to several weeks for complex ones, with molds adding time on new 3D designs.
Silver looks the same on a shop shelf whether it is sterling, plated brass or something in between. That is why check
READ FULLA stand collar can sit well on one customer and choke another. A “linen” tag can hide a fiber that shrink
READ FULLFrog buttons are the knotted loop-and-button closures known in Chinese as pankou (盘扣). A pankou is made of two pa
READ FULL